INSIGHTS FROM PRACTICE
Case Studies & Downloads
Ten case studies show how production teams capture machine states, investigate time losses and evaluate improvement measures. All project reports are available as English PDFs and detailed web pages. The additional solution overview explains the technology, requirements and implementation.
Which case study addresses your question?
CNC manufacturing: Investigate idle time between jobs, shift changes and the causes of downtime.
Expanded metal manufacturing: Understand stroke performance, interruptions and deviations from the plan in the context of each order.
Laser cutting: Identify losses from setup, loading, material waiting, microstops and downtime during cutting operations.
Industrial equipment manufacturing: Analyze idle time, setup losses, microstops and shift performance across a large CNC fleet.
Injection molding: Separate productive molding from setup, engineering work, waiting and recurring interruptions.
CNC & sheet metal manufacturing: Reveal waiting between operations, setup-readiness gaps and recurring interruptions across a mixed machine fleet.
Gas-safety manufacturing: Identify waiting, recurring stops, setup losses and lost productive time across a mixed-age machine fleet.
Cable extrusion: Understand productive extrusion, idle periods, setup-related losses and recurring line stops in continuous production.
Press brake manufacturing: Analyze productive bending, setup and changeover time, waiting periods, microstops and downtime.
Cable stranding: Identify reel and material waiting, setup losses, microstops and downtime during stranding operations.
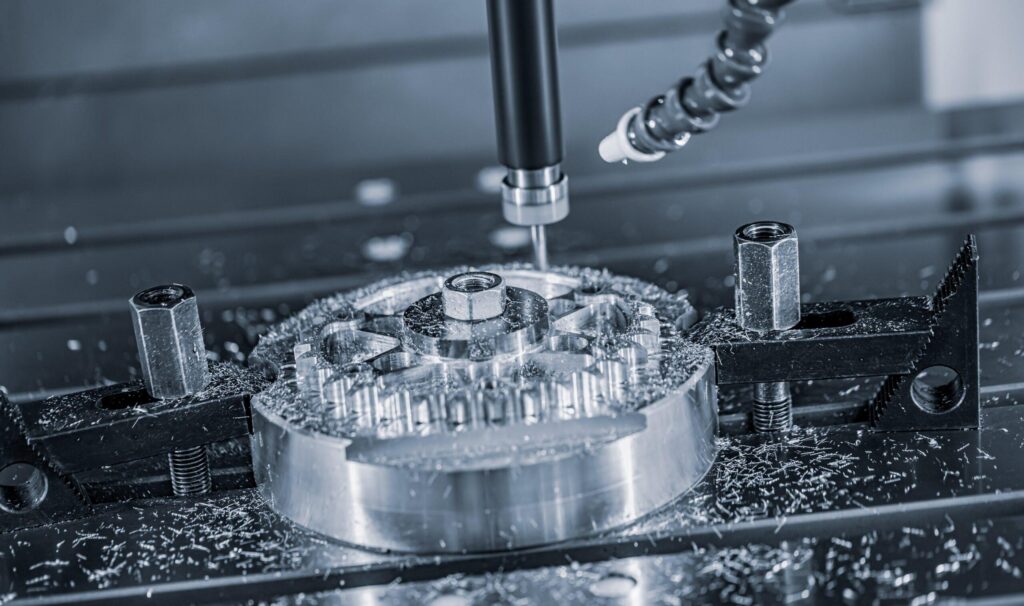
CASE STUDY · CNC MANUFACTURING
CNC Monitoring in Precision Tool Manufacturing
25 CNC machines operating across three shifts: External sensors make productive time and idle time visible. The case study reports 36.83% less idle time following process improvements. Read the CNC case study online →
Sensor installation took an average of 16.8 minutes per machine and was carried out during planned changeovers without PLC access. Signal validation and ERP/BDE integration added reliable machine states and order context to the data collection. The 4,083 additional productive machine-hours are an annualized figure for all 25 machines combined.
25 CNC MACHINES · ENGLISH PDF
↓ CNC case study PDF
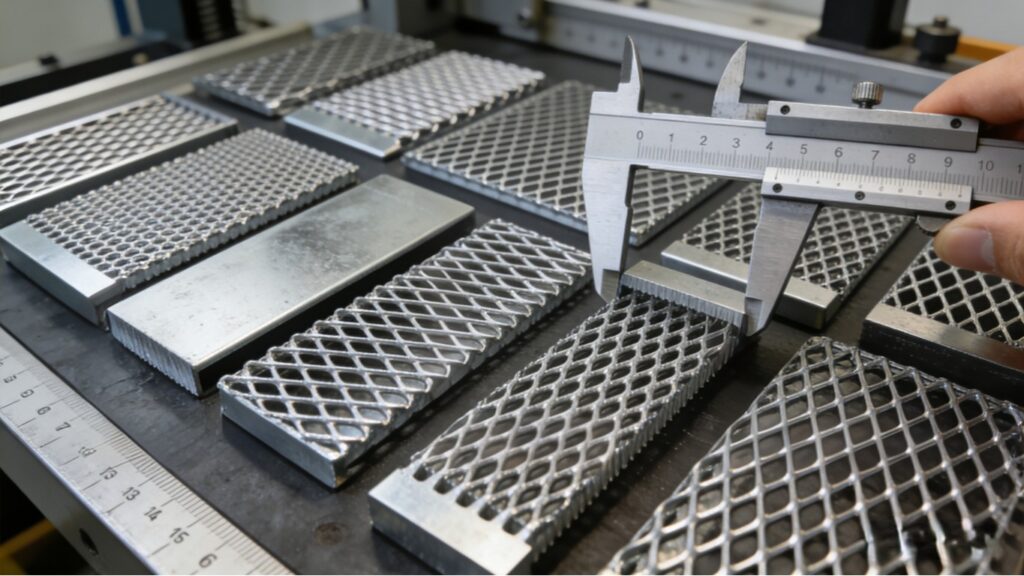
CASE STUDY · EXPANDED METAL
Targeted Monitoring of Stretching Machines
15 stretching and cutting machines operating across three shifts: After three months of operational improvements, the reported share of nonproductive time fell from 49.7% to 33.4%. The study shows the relationship between stroke performance, interruptions and planning. Read the stretching machine case study online →
Sensor installation without changes to the PLC took 15–20 minutes per machine; learning and validation phases followed separately. The share of nonproductive time fell by 16.3 percentage points, equivalent to approximately 32.8% relative to the baseline. The estimated 2,823 additional machine-hours per year apply to all 15 machines combined and were not measured directly over a full year.
15 MACHINES · ENGLISH PDF
↓ Stretching machine PDF
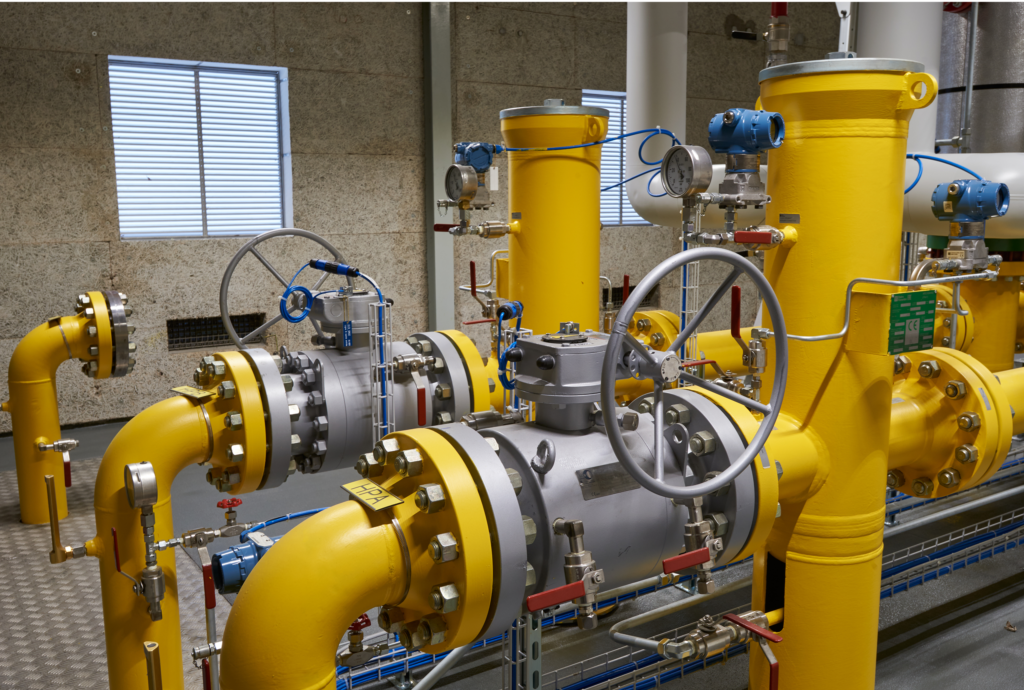
CASE STUDY · GAS-SAFETY MANUFACTURING
Gas-Safety Machine Monitoring
118 production machines built between 1998 and 2014: External sensing makes productive time, idle periods and recurring production losses visible across a mixed-age machine fleet. The customer reported 28.5% higher productivity. Read the gas-safety case study online →
External AVA sensors capture acoustic and vibration signals without requiring PLC access for the basic monitoring layer. Typical sensor installation was approximately 15 minutes per machine. In the operating model, idle time falls by 45%, while the calculated annual capacity scenario corresponds to 121,068 additional productive machine-hours across the 118-machine fleet.
118 MACHINES · ENGLISH PDF
↓ Gas-safety case study PDF
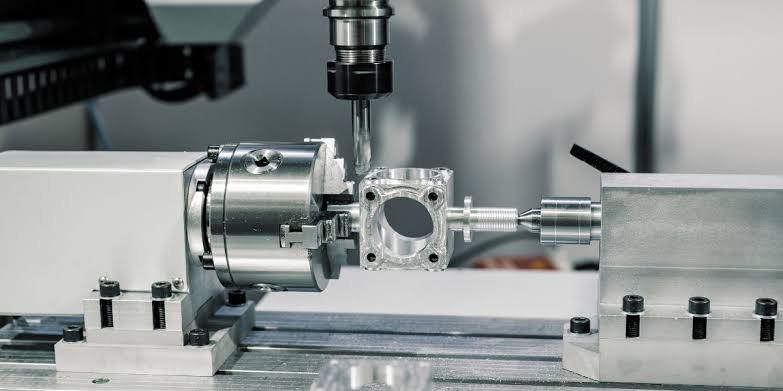
CASE STUDY · PRECISION CONTRACT MANUFACTURING
CNC and Sheet Metal Monitoring
20 production machines operating across three shifts: WatchMen makes waiting between jobs, recurring interruptions and setup-readiness losses visible across a mixed CNC and sheet-metal fleet. The customer reported 30% higher productivity. Read the CNC and sheet metal case study online →
AVA sensors and WatchMen provide one monitoring layer across machines from different generations without relying on access to every machine's PLC. In the operating model, productive share rises from 60.0% to 78.0%, corresponding to a calculated 21,600 additional productive machine-hours per year across the 20-machine fleet. Novo AI
20 PRODUCTION MACHINES · ENGLISH PDF
↓ CNC & sheet metal case study PDF
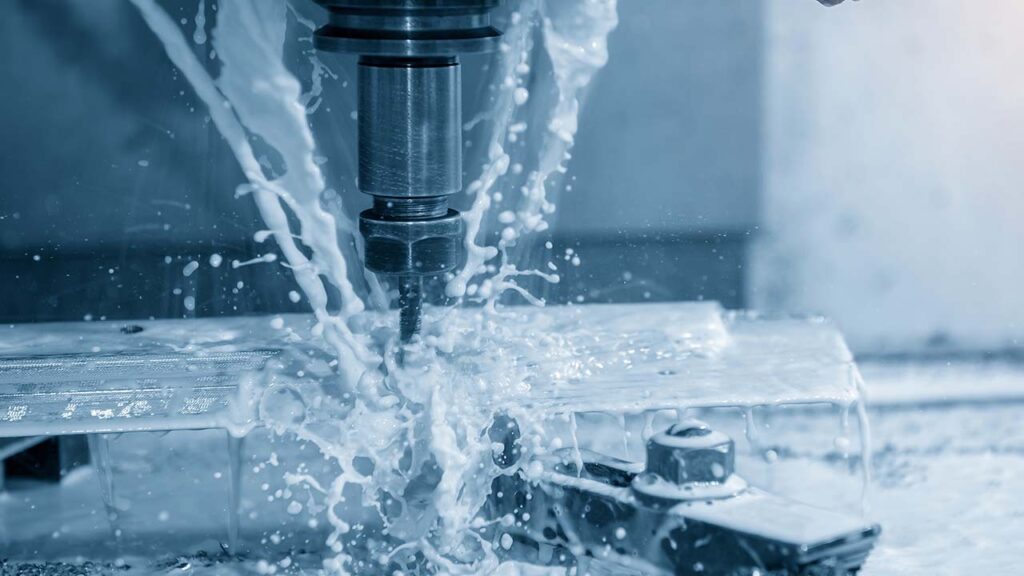
CASE STUDY · INDUSTRIAL EQUIPMENT
CNC Monitoring in Industrial Equipment Manufacturing
125 CNC turning and milling machines operating across three shifts: WatchMen makes idle time, microstops, setup losses and downtime visible across the fleet. The customer reported 27% higher productivity. Read the CNC case study online →
Machine-state data reveals waiting for material, tools, approvals and the next order while also making recurring interruptions and shift differences comparable. In the calculation model, productive share rises from 60.0% to 76.2%, corresponding to an estimated 121,500 additional productive machine-hours per year across the 125-machine fleet.
125 CNC MACHINES · ENGLISH PDF
↓ CNC industrial equipment PDF
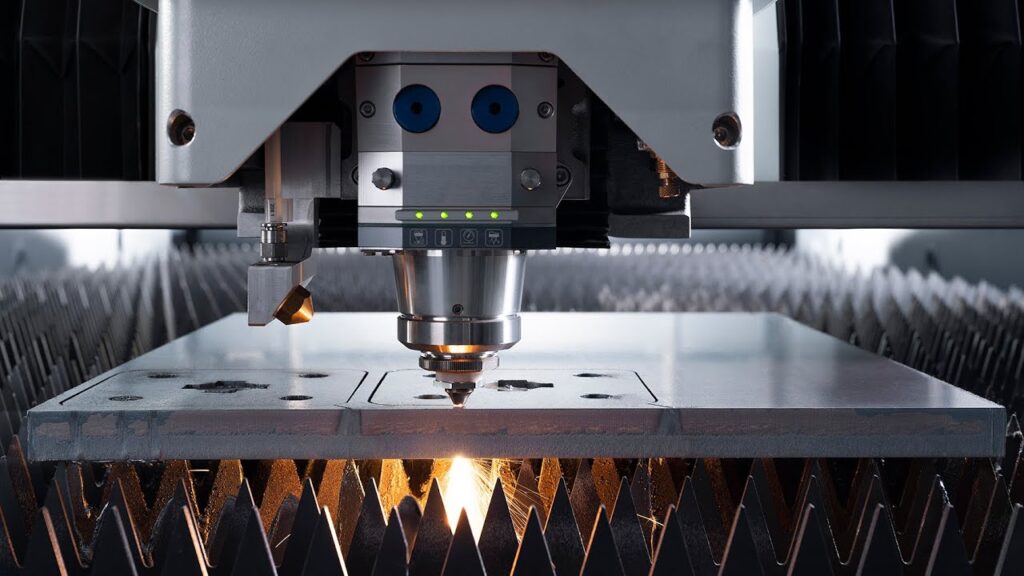
CASE STUDY · SHEET METAL MANUFACTURING
Laser Cutting Machine Monitoring
136 machines used for laser cutting: WatchMen makes productive cutting, idle time, setup, loading, microstops and downtime visible across the machine fleet. The customer reported 26.4% higher productivity. Read the laser cutting case study online →
External retrofit sensors create a common monitoring layer across different machine generations without requiring basic PLC access. Sensor installation took approximately 15 minutes per machine. In the operating model, idle time fell by 39.29%, while the estimated annual capacity gain was 71,808 productive machine-hours across the project scope. The annual figure is a modeled capacity estimate, not a full year of directly measured additional output.
136 MACHINES · ENGLISH PDF
↓ Laser cutting case study PDF
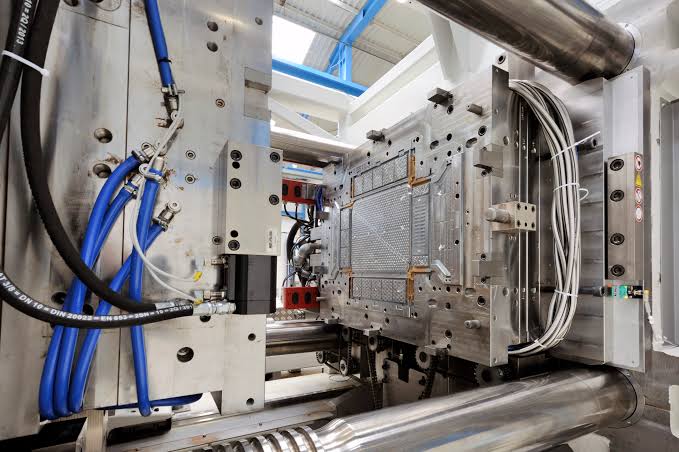
CASE STUDY · PRECISION MOLD MANUFACTURING
Injection Molding Monitoring
40 injection molding machines built between 2003 and 2017: Machine-state and cycle data make productive molding, setup, engineering work, waiting and recurring interruptions distinguishable. The customer reported 31.13% higher productivity. Read the injection molding case study online →
External sensors capture machine behavior without requiring PLC access for the basic monitoring layer, with approximately 15 minutes of sensor installation per machine. In the operating model, idle time falls by 55.56%. The modeled improvement corresponds to approximately 24,904 additional productive machine-hours per year across the monitored fleet.
40 MACHINES · ENGLISH PDF
↓ Injection molding case study PDF
CASE STUDY · CABLE MANUFACTURING
Stranding Machine Monitoring in Cable Manufacturing
18 stranding machines from mixed machine generations: WatchMen makes productive stranding, idle time, reel and material waiting, setup losses, microstops and downtime visible. The customer reported 29.23% higher productivity. Read the stranding machine case study online →
External Novo AI sensors created a common monitoring layer across all 18 stranding machines without requiring basic PLC access. In the modeled production scenario, idle time was reduced by 43.75%. The corresponding annual capacity estimate is approximately 10,522.8 additional productive machine-hours across the monitored fleet. This represents released production capacity rather than a full year of directly measured additional cable output.
18 STRANDING MACHINES · ENGLISH PDF
↓ Stranding machine case study PDF
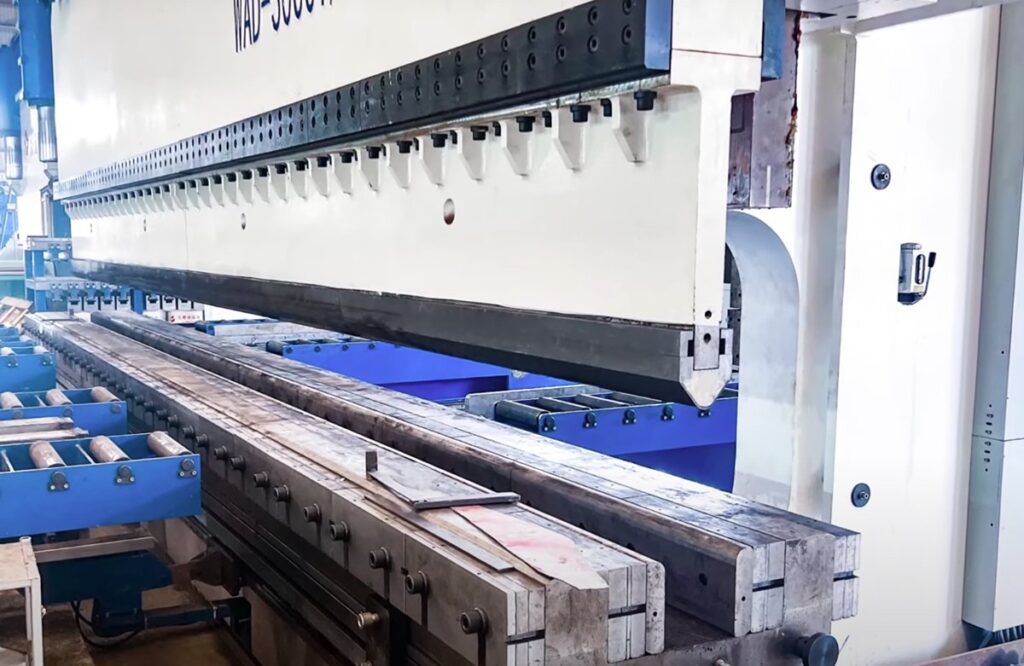
CASE STUDY · SHEET METAL FABRICATION
Press Brake Monitoring in Sheet Metal Manufacturing
36 press brakes in sheet metal production: WatchMen makes productive bending, setup and changeover time, waiting periods, microstops and downtime visible. The case study shows where productive machine time is lost between bending operations. The customer reported 28.76% higher productivity. Read the press brake case study online →
External retrofit sensors create a common monitoring layer across 36 press brakes without requiring intervention in the machine control system. Machine-state and cycle data make productive bending, setup phases, waiting periods and recurring interruptions visible, helping production teams identify where capacity is lost and compare performance over time.
36 PRESS BRAKES · ENGLISH PDF
↓ Press brake case study PDF
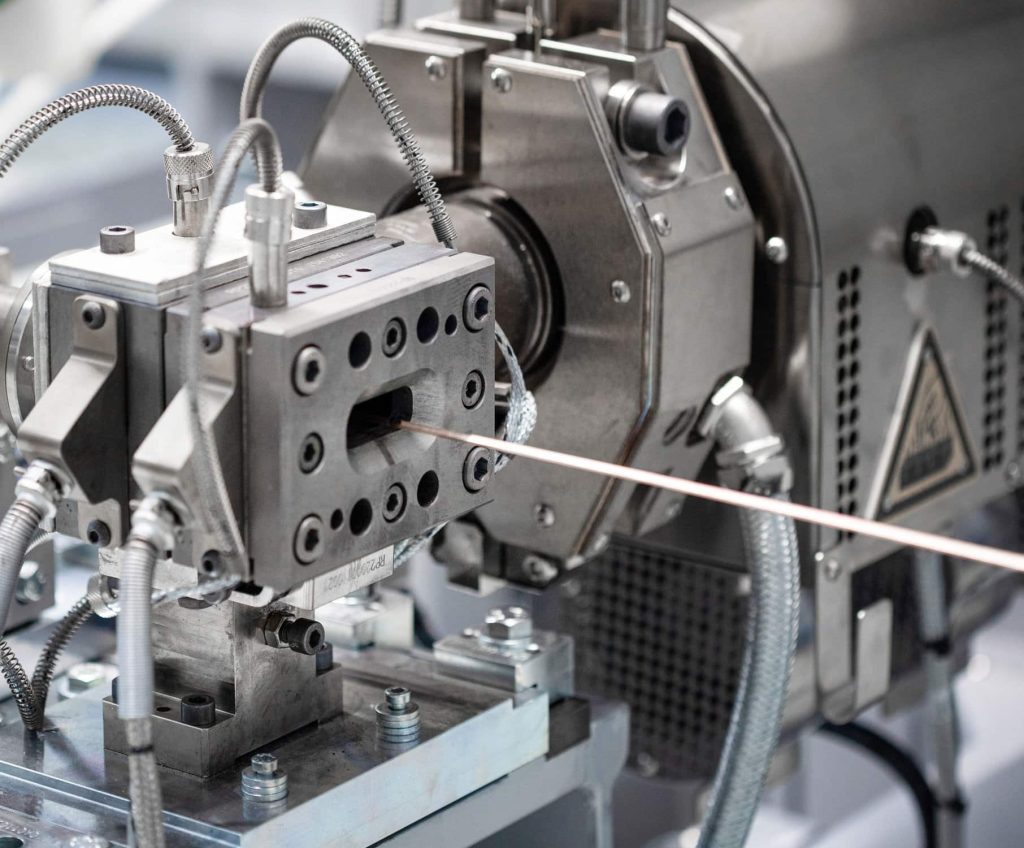
CASE STUDY · CABLE MANUFACTURING
Cable Extrusion Monitoring
13 cable extrusion lines: WatchMen makes productive extrusion, idle periods, line stops and recurring losses around continuous production visible. The case study shows how machine-state data helps distinguish actual production time from hidden losses before, during and after the run. The customer reported 27.6% higher productivity. Read the cable extrusion case study online →
External retrofit sensors create a common monitoring layer across existing extrusion lines without requiring basic PLC access. WatchMen makes productive running time, idle phases, stops and changes in process behavior visible so that production teams can investigate where capacity is being lost around an otherwise continuous process. novoai.de
13 EXTRUSION LINES · ENGLISH PDF
↓ Cable extrusion case study PDF
Putting Case Studies into Context
These case studies are intended for production managers, production planners and those responsible for digitalizing existing machines. They show how continuous machine data acquisition creates transparency and supports decisions. The documented changes resulted from the combination of data analysis and operational measures.
From Machine States to Reliable Metrics
Runtime, idle time and downtime answer different questions. First, define which time counts as productive and which reference period is used. Better utilization does not automatically mean an equally large increase in OEE: OEE also accounts for performance and quality. The OEE calculation based on availability, performance and quality explains this distinction.
Comparing Percentages and Annualized Figures
For the stretching machines, the decrease from 49.7% to 33.4% represents a reduction of 16.3 percentage points, or approximately 32.8% relative to the baseline. The CNC case study reports a different metric: the reduction in idle time. These figures therefore cannot be equated directly. Check which machines, periods and process measures are included in each study's analysis.
Four Questions for Your Machine Fleet
- Goal: Which downtime, bottlenecks or unused capacity would you like to understand?
- Data: Which machine states can be measured, and which order, quantity or quality data is missing?
- Comparison: Which shifts, products and reference periods enable a fair before-and-after comparison?
- Measures: Who evaluates the results and checks whether changes have a lasting effect?
Frequently Asked Questions About Our Case Studies
Does machine monitoring work without PLC access?
In both projects described, machine states were captured using external retrofit sensors without accessing the PLC or machine controls. Which signals can be reliably analyzed on a specific machine depends on the machine type and process and must be checked during setup.
How long does it take to retrofit a machine?
The CNC case study reports an average of 16.8 minutes for sensor installation. For the stretching machines, 15–20 minutes per machine are reported. These figures refer to installation in the respective project. Learning phases, validation and integration into operational workflows should be considered separately.
Are machine utilization and OEE the same thing?
No. Machine utilization describes the use of a machine relative to a defined reference period. OEE combines availability, performance and quality. Machine states make time losses visible; a complete OEE calculation also requires appropriate performance and quality data.
Can the results be transferred to other companies?
The case studies document individual applications. Results depend on factors including the starting conditions, shift model, product mix and process changes implemented. Annual figures for additional usable hours are extrapolations. Therefore, compare reference periods, measurement periods and measures before assessing the potential for your own operations.
Publisher: Novo AI GmbH. This overview is based on the published project descriptions for CNC manufacturing and expanded metal manufacturing. Full details of each project can be found in the linked studies.